


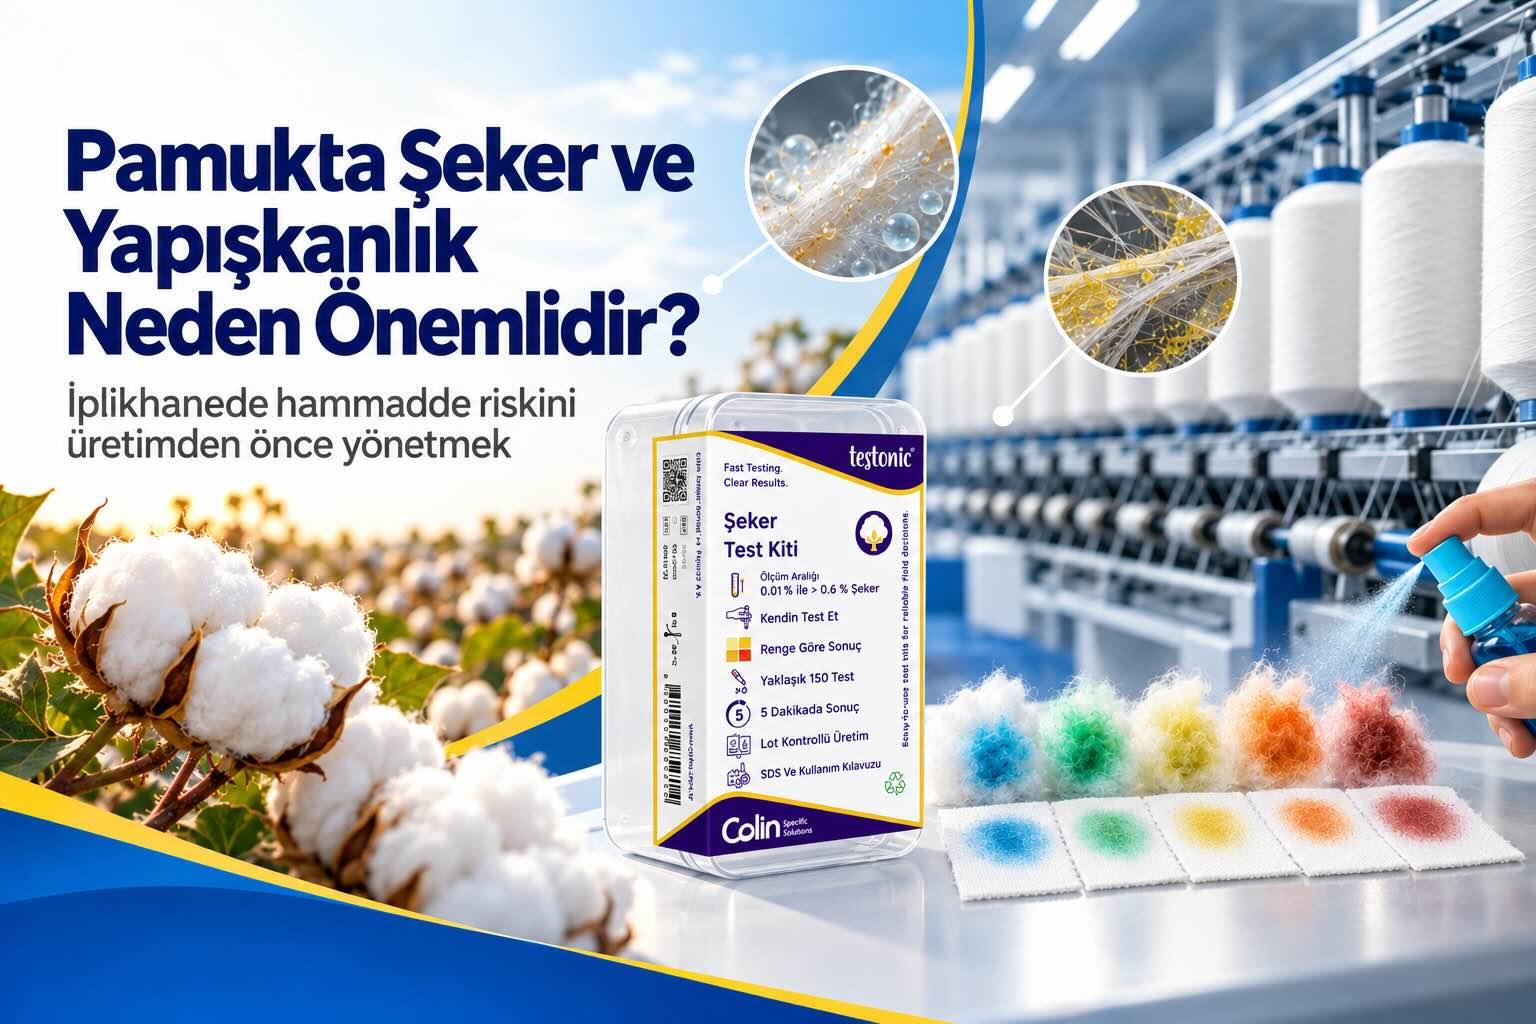
Technical Overview
Raw cotton may appear acceptable in terms of colour, appearance and conventional fibre properties while still carrying a sugar load that differs considerably from lot to lot. As sugar load increases, the risk of stickiness, deposits on machinery, increased cleaning demand, process instability and production losses may also increase. Sugar content and actual stickiness, however, are not identical concepts. The source and composition of the sugars, their distribution on the fibre and the temperature and relative-humidity conditions in the spinning mill can all influence actual processing behaviour. The most effective approach is therefore to compare each new cotton lot with proven reference lots and relate the result to actual mill performance.
Contents
Why Does Cotton Quality Control Begin in the Field?
By the time cotton reaches the spinning mill, much of its quality history has already been established. Variety, growing conditions, harvesting time, insect pressure, harvesting practices, ginning, baling and storage can influence not only conventional fibre properties but also the surface contamination and sugar profile of the incoming raw material.
For this reason, assessing a cotton lot solely in terms of fibre length, fineness, strength, colour or trash content may not always be sufficient. Sugar load capable of contributing to processing stickiness may create a major operational difference between two lots that otherwise appear similar.
The effect is frequently seen not in the visual appearance of the cotton but in the behaviour of the machinery: irregular fibre flow, deposits on machine surfaces, shorter cleaning intervals, increased ends-down or unexpected lot-to-lot process variation.

Is this cotton merely within specification, or is it also capable of running consistently in our mill?
Where Does Sugar on Cotton Come From?
Sugar load on cotton lint does not have a single source. A positive or elevated sugar result should therefore not automatically be attributed to one agricultural or processing cause.
Natural Plant Sugars
The metabolism of the cotton plant naturally involves carbohydrates. Sugars such as glucose, fructose and sucrose may be associated with fibre development, maturity and plant-derived residues.
The presence of normal physiological sugars does not by itself mean that the cotton will cause a processing problem. They nevertheless contribute to the overall sugar profile and should be considered together with fibre maturity and other raw-material characteristics.
Honeydew from Aphids and Whiteflies
One of the major concerns in sticky-cotton management is contamination by sugary secretions produced by phloem-feeding insects such as cotton aphids and whiteflies. These insects can deposit honeydew containing various sugars onto the cotton surface.
Honeydew contamination is not necessarily uniform. Different areas of the same field, bale or lot may contain different levels of contamination, making representative sampling particularly important.
Not all sugars produce identical sticking behaviour. Total sugar load is a valuable screening parameter, but actual mill behaviour can vary according to sugar composition and distribution on the fibre.

Are Sugar Load and Cotton Stickiness the Same Thing?
No. This distinction is critical for textile and chemical engineers.
A sugar test evaluates the sugar load carried by the cotton. Stickiness describes the actual operational behaviour that occurs when these materials interfere with fibre processing and machinery.
An elevated sugar load is therefore an important risk indicator, but two cotton lots with similar sugar results do not necessarily have to behave identically in the spinning mill.
Actual processing behaviour may also depend on:
- Sugar composition,
- Distribution of sugar deposits on the fibre,
- Origin of honeydew contamination,
- Relative humidity and temperature,
- Moisture equilibrium of the cotton,
- Machine-surface and operating conditions,
- Other cottons in the blend,
- The amount of material processed and the cumulative development of deposits.
Instead of “high sugar = this cotton cannot be processed”, use “the sugar load is higher than our proven reference; this lot requires closer monitoring for stickiness and process stability.”
How Can a High Sugar Load Develop into a Problem Chain in the Spinning Mill?
A characteristic feature of sugar-related processing problems is that the effect may not remain confined to one machine. Sticky materials can move through the process with the fibre and gradually build up on machine surfaces.
Early signs may appear during opening and cleaning as irregular fibre movement, increased accumulation of fibre and dust, or shorter cleaning intervals.
At subsequent stages, deposits on rollers, aprons or contact surfaces may interfere with fibre control. This can increase both maintenance demand and the frequency of operator intervention.
The cumulative result may be more cleaning, additional stoppages, ends-down, greater variability and lower production efficiency.

Why Should a New Cotton Lot Be Compared with a Reference Lot?
A single result interpreted without production context provides only limited information. A stronger mill approach is to compare each new lot against cotton that has previously processed reliably on the same equipment.
A good reference lot is not merely cotton with a low sugar result. It should also have a proven production history with acceptable cleaning intervals, no recurring stickiness problem, stable running conditions and the required yarn quality.
Where possible, the reference should be a profile based on several successful lots rather than one individual bale or batch.

How Should the Testonic Sugar Test Result Be Interpreted?
The Testonic Sugar Test Kit classifies approximate sugar load in raw cotton by colour. The result should be used primarily to classify raw-material risk and determine the next control step rather than as a stand-alone pass/fail decision.
| Colour | Approximate Sugar Load | Engineering Approach |
|---|---|---|
| Blue | < 0.1% | Very low sugar load. Together with proven processing performance, it can contribute to establishing a suitable reference profile. |
| Greenish Blue | 0.1–0.3% | Low sugar load. Record together with normal mill performance for future lot comparison. |
| Yellow-Green | 0.3–0.6% | Moderate sugar load. Compare against reference lots and monitor cleaning intervals and processing behaviour more closely. |
| Orange | 0.6–1.0% | Pronounced sugar load. Separate lot monitoring, controlled production verification and more careful process and cleaning planning are advisable. |
| Reddish | > 1.0% | High sugar load. Raw-material acceptance, lot segregation, supplier evaluation and full-scale production strategy should receive priority review. |
What Production Decisions Should Follow the Test Result?

With low sugar load comparable to successful references, the standard process can normally continue while the result is retained as part of the mill's reference database.
At moderate levels, the lot should be monitored more closely for deposits, cleaning intervals, operator intervention and ends-down.
With pronounced or high sugar load, a controlled production verification may be preferable before committing the complete lot to full-scale production. Segregation, increased inspection and cleaning frequency, environmental stability and supplier follow-up can all form part of the risk-management plan.
Why Do Relative Humidity and Temperature Matter?
Sugar load should not be considered only as a chemical quantity. Many sugars have hygroscopic properties and interact with environmental moisture.
The same cotton can therefore show different processing behaviour under different conditioning conditions. In sugar-loaded cotton, changes in relative humidity may influence surface tackiness and transfer to machinery.
This does not mean that the solution is simply to minimise humidity. Excessively dry conditions may introduce other processing problems, including static electricity and altered fibre behaviour.
The better engineering approach is to keep the mill's validated conditioning conditions stable and record relative humidity and temperature when comparing problematic and reference lots.
How Can Sugar Results Be Integrated into Supplier and Incoming-Raw-Material Control?
A single sugar result describes one sample. Repeated testing linked with production data creates a much more valuable supplier-performance system.
Useful records include supplier and origin, bale or lot identification, sugar class, machinery-cleaning frequency, stoppages, ends-down, temperature and humidity conditions and final yarn performance.
Once sufficient data has been collected, purchasing can evaluate not only the purchase price of cotton but also hidden operating costs associated with cleaning, downtime, reduced efficiency and quality variation.
Where Does the Testonic Sugar Test Kit for Cotton Fit into This System?
Testonic Sugar Test Kit – For Cotton is intended to support comparison of raw-cotton lots according to sugar load and to make potentially higher-risk material visible before full-scale production.
Its primary operational value is helping mills answer questions such as:
- Does the new lot differ from our proven references?
- Do higher sugar results coincide with increased stickiness or machinery contamination in our mill?
- Does the same pattern recur for a particular supplier or origin?
- Can this lot follow the standard production plan, or does it require closer observation?
- Should cleaning or process monitoring temporarily be intensified?
- How does sugar level relate to actual yarn quality and productivity?
Used in this way, the kit becomes more than a one-time laboratory or field check. It becomes part of incoming raw-material control, lot classification, supplier-performance evaluation and pre-production risk management.
Frequently Asked Questions
Conclusion
Sugar load is a raw-material variable that may be difficult to see on cotton but highly visible once the material enters the spinning process.
Stickiness, machinery deposits, increased cleaning demand, downtime and process instability should not be viewed solely as spinning-department problems. They can also be consequences of incoming-raw-material variability, lot management and supplier consistency.
The technically correct approach is not to conclude that “cotton containing sugar is poor cotton”. Instead, mills should identify sugar load early, compare new material against successful reference lots, control environmental conditions and link analytical results with actual production performance.
With this approach, sugar testing becomes more than an analytical result. It becomes a decision tool connecting cotton purchasing and incoming quality control with real spinning-mill performance.
Start Managing Yarn Quality at Raw-Material Acceptance
Compare every new cotton lot with proven reference materials and evaluate sugar load together with machinery behaviour and actual yarn performance to build a mill-specific cotton quality profile.

